The core idea of this page: a seal is a controlled melt-and-press operation. Three parameters — temperature, pressure and dwell — must sit inside a window set by the sealant, and the window narrows with contamination, film lot variation and machine wear. Seal integrity is the practice of proving the pack sits inside that window, not of looking at it.
How a heat seal forms
The sealant layer
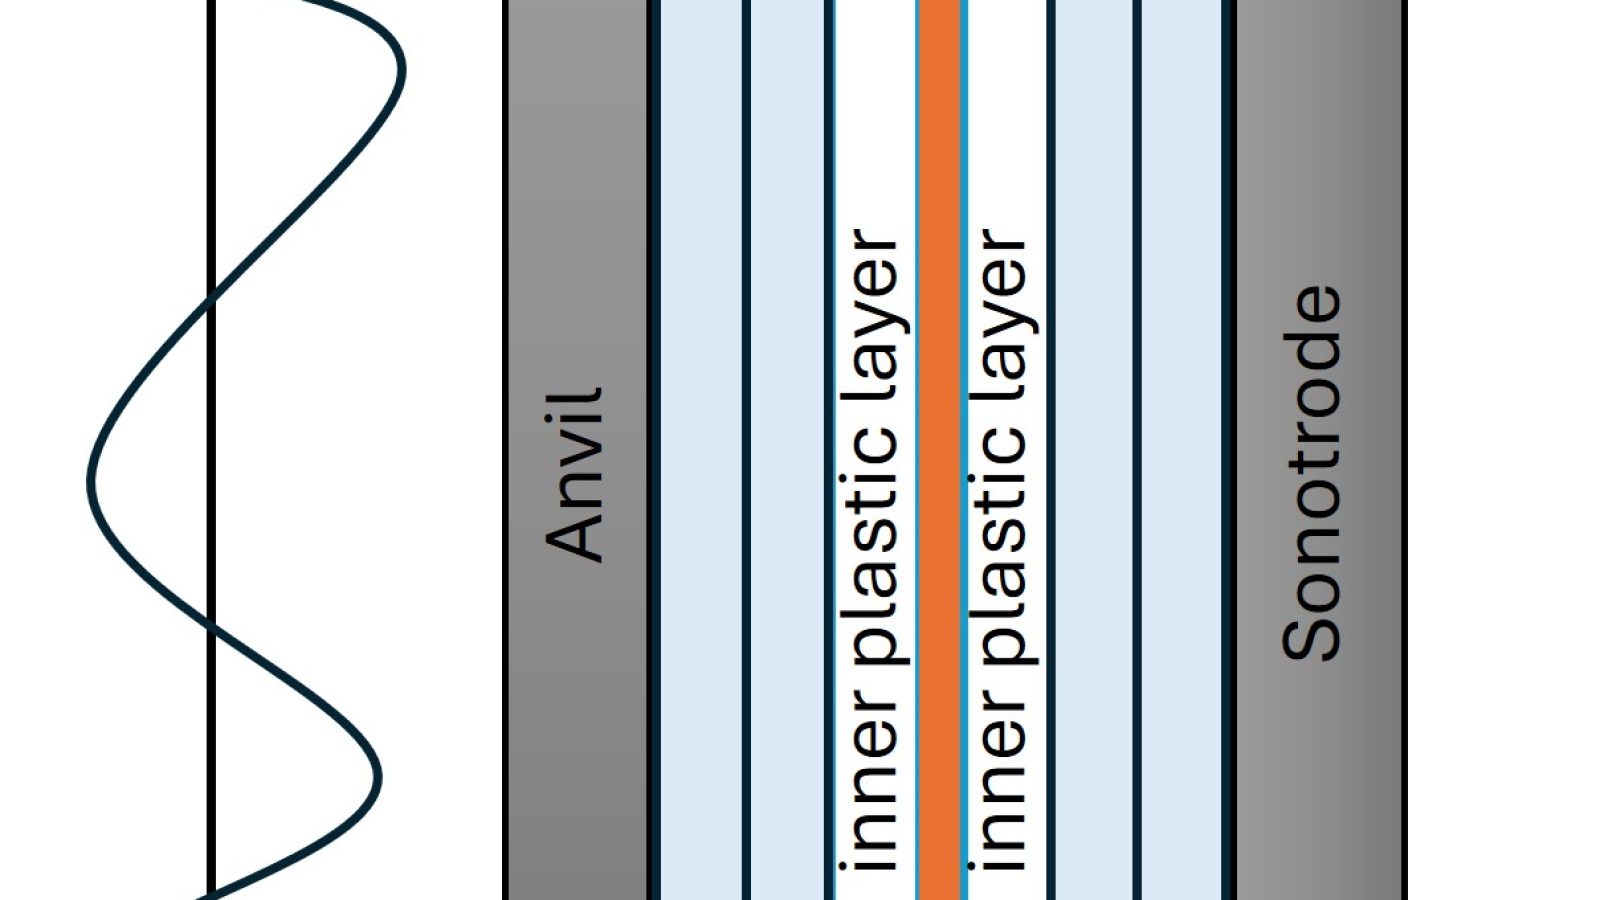
Only the sealant layer melts. Its melting range, thickness and contamination tolerance define the window. A seal that looks continuous can have zero peel strength if the sealant did not reach its melting range across the full area.
Temperature, pressure, dwell
Temperature drives the melt, pressure closes the interface, dwell gives heat time to penetrate. The three trade off: a hotter jaw can run a shorter dwell, but a narrower window for film variation. Serrated jaws concentrate pressure and tolerate contamination better than flat jaws but can thin the seal.
Cooling
A seal is not finished when the jaw opens. The sealant must cool under pressure or it can be pulled apart by the film tension as the pack moves. On high-speed lines, insufficient cooling is a common hidden cause of weak seals.
Failure modes that pass visual inspection
Channel leaks
A path through the seal caused by contamination, a wrinkle or a fold. Invisible to the eye and fatal in transit; only a leak test finds them.
Cold seal / incomplete melt
The seal looks closed but the sealant never fused. Peel strength is near zero; the pack survives handling and fails under load.
Wrinkle and fold-over
Film folds in the seal area create a rigid double layer that cannot be compressed evenly, producing a leak path at the fold edge.
Contamination
Product, dust or liquid in the seal zone. Powders and sticky liquids are the classic offenders; the fix is machine-side (squeeze, nozzle, clean seal zone) more often than film-side.
Test methods
Visual inspection
Useful for gross defects and useless for channels. It should be a screening step, never the acceptance test.
Dye penetration
A dye solution drawn into a channel under vacuum or pressure. Fast, cheap, destructive, and good at finding channel leaks along the seal.
Burst and creep testing
Pressurise the pack until it fails, or hold a pressure and watch for creep. Measures the weakest point of the whole pack, including fitments.
Vacuum decay / pressure decay
Non-destructive for some pack types: measure the pressure change in a chamber or inside the pack. Good for production sampling.
Peel strength
Pull the seal apart at a controlled rate and record force. This is the test that exposes cold seals and parameter drift before they become customer complaints.
Establishing the seal window
Do not inherit a parameter set from a data sheet. Run a trial that varies temperature, dwell and pressure across a grid, then measure peel strength and leak rate at each point. The passing region is rarely a point; it is an area, and the correct setting is its centre. A setting chosen at the edge of the region runs until the first cold morning or the first new film lot, then fails.
Repeat the trial after any change of film lot, sealant supplier, jaw coating or product recipe, and record the resulting window per format.
Jaw maintenance
Seal quality degrades through jaw wear long before anything breaks. Check flatness with a straight edge, parallelism across the width, coating condition and heater uniformity with a thermal image. Product build-up on the jaw face is a contamination source and also an insulation layer, so a cleaning interval belongs in the preventive-maintenance plan, not in the operator's judgement.
Sampling and acceptance criteria
Define sample size per shift and per format, the test methods per pack type, and numeric pass limits. Record the values; a pass/fail tick with no number cannot show drift. For critical products, run a challenge test with deliberately contaminated seals to prove the test method can actually detect a bad seal.
Hot tack and why it matters at speed
Hot tack is the strength of a seal while it is still molten. A film with good final peel strength but poor hot tack fails at high speed, because the pack is pulled away from the jaw before the seal has cooled. This is why a laminate that works on a slow machine can fail on a fast one with identical temperature settings, and why hot-tack data belongs in the film specification for any line running above a few cycles per second.
Records and traceability
Keep seal parameters, film lot, test results and any parameter change against the production batch. When a customer complaint arrives months later, the question is always "what was different that day" — and the answer is only available if the records exist. A one-page seal record per shift costs minutes and settles arguments that otherwise end in a recall.
Fixing a drifting seal window
When leak rates rise: check jaw temperature uniformity across the seal width, jaw flatness and parallelism, dwell timing against the machine's actual cycle, and film lot. Then re-establish the window with a design-of-experiment style trial — vary temperature and dwell, measure peel strength and leak rate, and choose the centre of the passing region rather than an edge.
Verification checklist
Confirm: seal parameters documented per format and locked; jaw temperature measured across the width, not at one point; cooling verified at line speed; leak and peel tests with numeric limits and sample sizes; film lot recorded per batch; and a re-validation trigger written for film, product or machine changes.
Source: Package testing — Wikipedia
"Package testing or packaging testing involves the measurement of a characteristic or property involved with packaging."
Frequently asked questions
Is a visual seal check enough?
No. Channels and cold seals pass visual inspection. Use a leak or peel test with numeric limits, and keep the visual check as a screening step.
Why do seals fail after hours of running?
Thermal drift, jaw wear, film lot change or product build-up on the jaws. Stability over a full shift is what the sustained run is meant to prove.
What is the most common cause of leakers?
Product contamination in the seal zone, followed by insufficient cooling and seal-parameter drift.
Related reading: doypack construction, FAT and SAT, site acceptance test, and the sealing and closing category.
Related guides
- Sealing Machines: Top 10 Tray Sealers Compared (2026) — Five automatic tray sealers compared across sealing capability, format…
- Sealing Machine Price Guide: Costs, Types & Buying Factors — Understand what a sealing machine quote should include, how machine ty…
- Tray Sealing vs Vacuum Chamber Sealing: Which Closure Fits Your Pack — Tray sealing and vacuum chamber sealing solve different closure proble…
- Heat Sealing vs Induction Sealing: Closing Methods Compared — Heat sealing welds film with heated elements; induction sealing welds …
- MAP vs Vacuum Skin Packaging: Sealing for Shelf Life — MAP gas-flushes a tray headspace; vacuum skin packaging draws the film…
- Modified Atmosphere Packaging (MAP) — modified atmosphere packaging replaces the air inside a pack with a ga…
- How a Tray Sealer Works — a tray sealer puts a filled tray into a die, pulls a lid film over it,…
- How Induction Sealing Works — induction sealing heats a foil liner inside a plastic cap by inducing …