The core idea of this page: a packaging line is designed from the product out, not from the machines in. Fix the product, pack format and realistic line rate first, then sequence primary, secondary and end-of-line machines, balance the line around its bottleneck, and define utilities, safety and acceptance before you buy anything.
Last updated: October 20, 2026. A packaging line that is specified machine-by-machine usually meets its brochure speed on day one and never again. This guide walks the design and integration path in the order that prevents the most expensive mistakes. For the machine categories referenced here, browse the Packaging Machinery topic.
Step 1 — Fix the product and the pack format
Every downstream decision is a consequence of what you are packing. Before any machine, write down: the product and its behaviour (viscosity, particulates, fragility, free-fall), the primary container (bottle, jar, pouch, tray, bag), the secondary pack (carton, case, shrink bundle) and the closure. A sauce that pumps easily warm may refuse the same nozzle cold, and a fragile product rules out a free-fall VFFS in favour of an HFFS or pre-made pouch line. See VFFS vs HFFS Packaging Machines when the primary format is still open.
Step 2 — Fix the rate you will actually run
Do not design to peak brochure speed. Design to a sustained rate over a full shift, stated as good packs per minute or per hour, and give yourself a defined headroom (commonly 10–20%) above your committed output. The number that matters is net output after stops, rejects and changeovers — that is the line’s availability, which the OEE calculation makes explicit. If you are unsure what a line should cost or deliver, start from How Much Does a Packaging Machine Cost?.
Step 3 — Sequence the machines
Lay the line out as primary → secondary → end-of-line, and only then choose each machine:
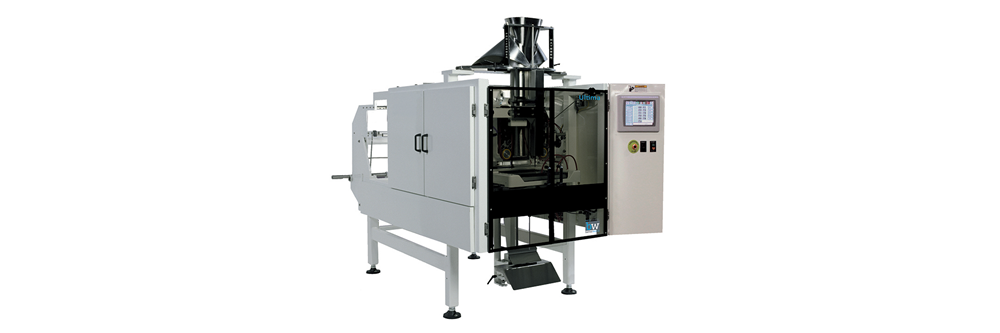
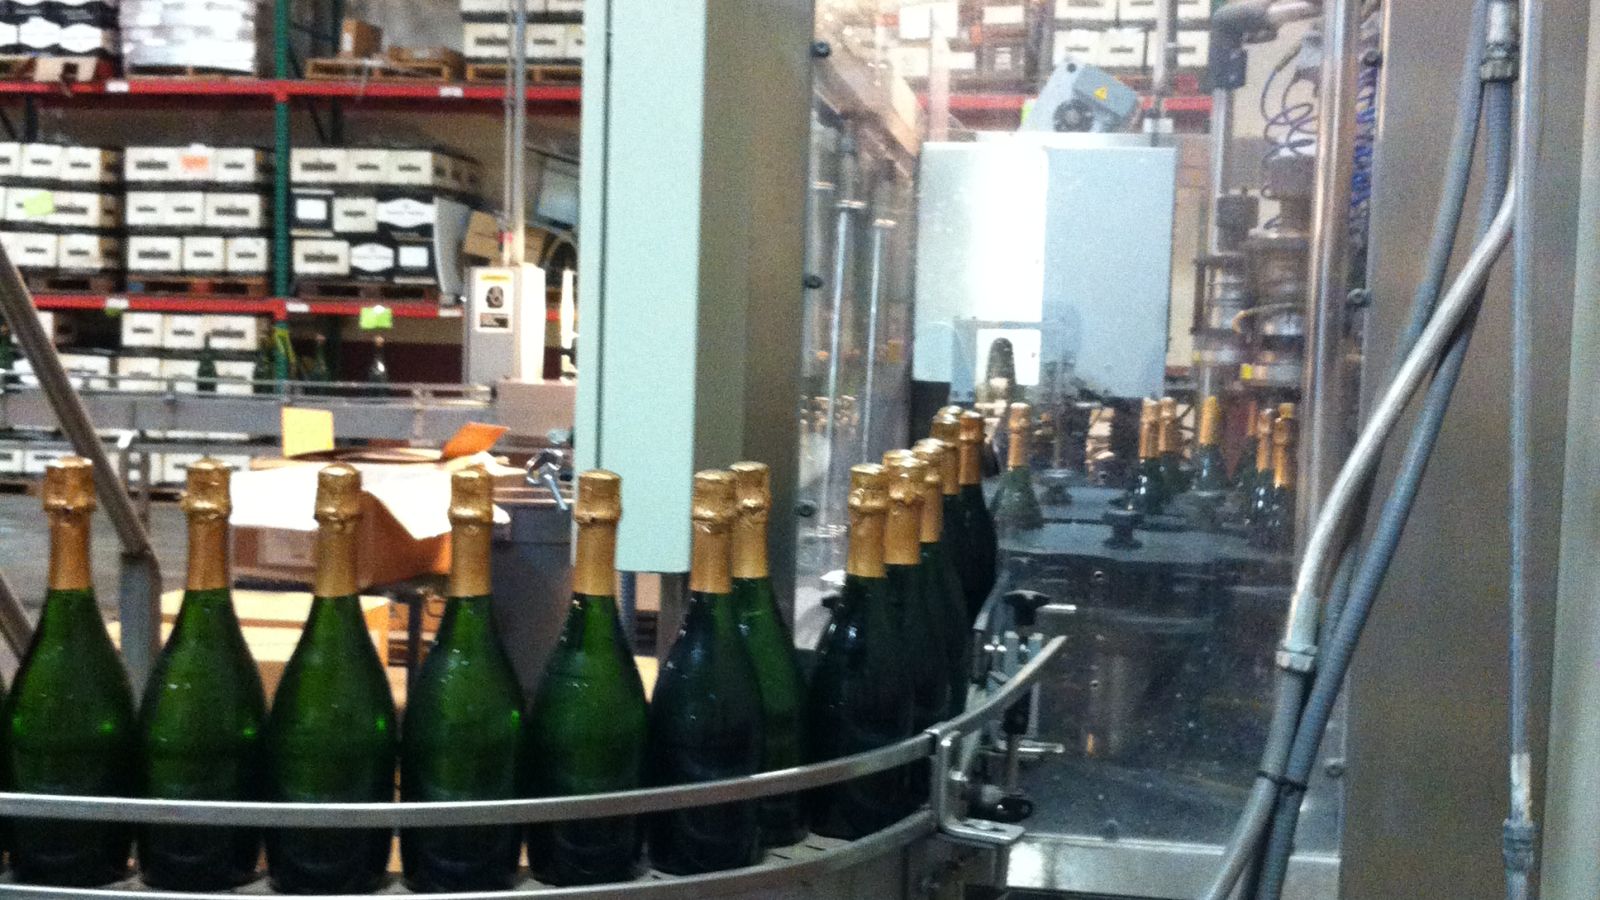
- Primary: the filler, doser, or form-fill-seal machine that makes the primary pack — this sets the line speed and is the least flexible to change later.
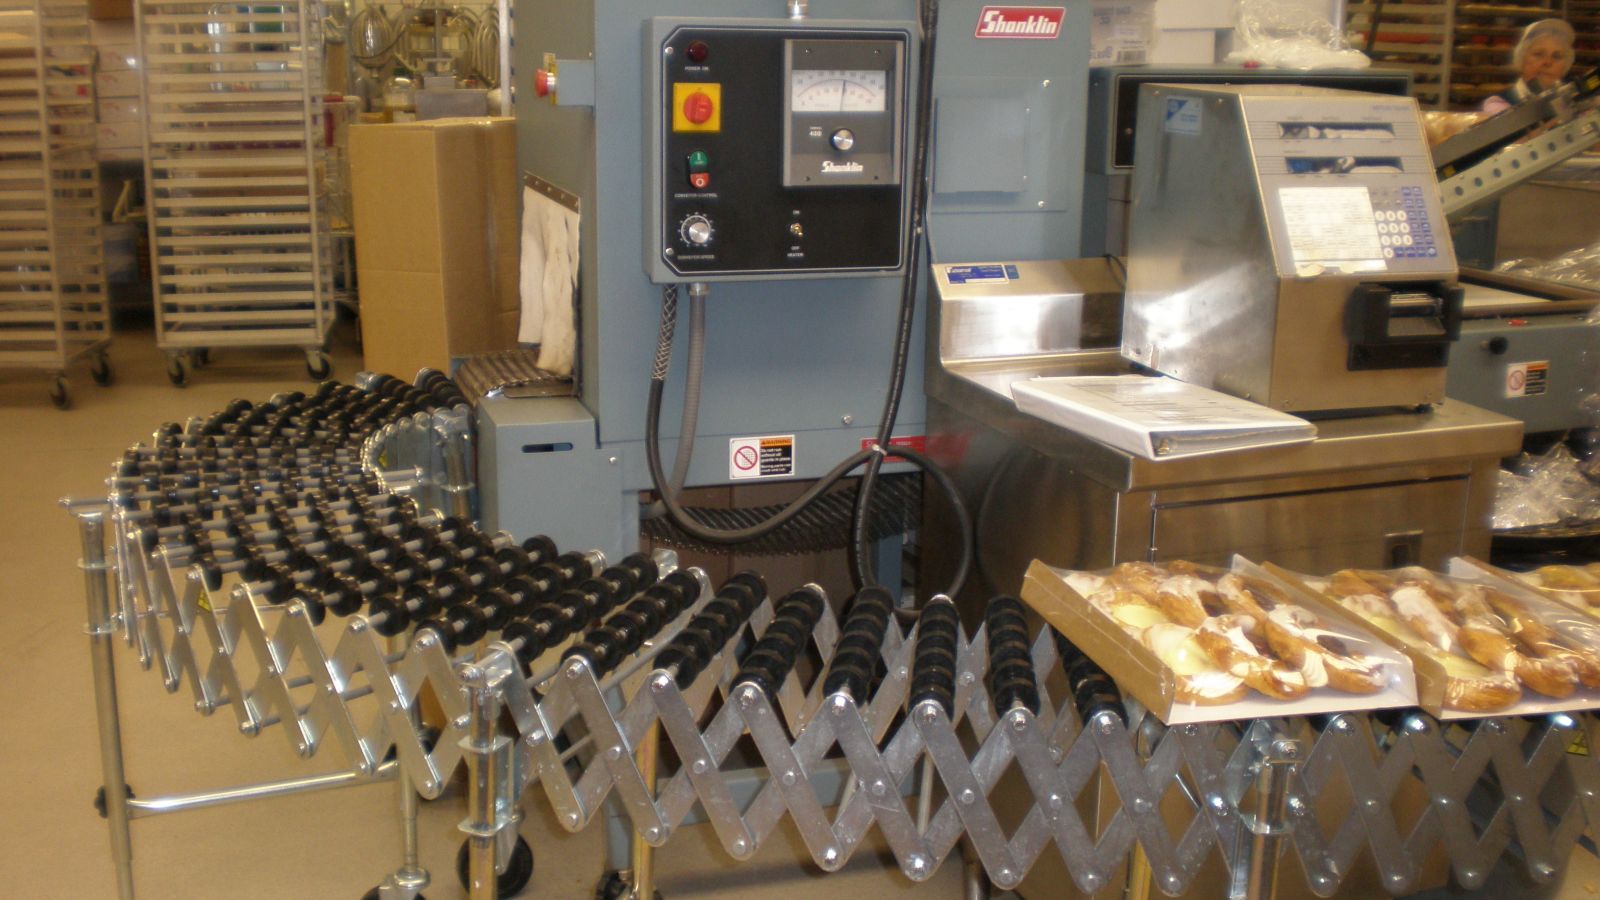
- Secondary: sealing, labeling, coding and inspection — sized to the primary output and to the reject handling they create.
- End-of-line: case packing, palletizing and load stabilization — see What Is an End-of-Line Packaging System? for the downstream view.
Step 4 — Balance the line around its bottleneck
Find the slowest machine and design buffers and accumulation around it, not around the fastest machine. Two practical rules: put accumulation upstream of a bottleneck so it never starves, and put inspection downstream of the operations that create defects so rejects are caught before they reach the end of the line. A line is as fast as its constraint — improving a non-constraint machine only builds inventory in front of it.
Step 5 — Utilities, layout and safety
- Utilities: compressed air, electrical supply, water and (for hygienic lines) steam and drainage. Undersizing air supply is a common cause of slow indexing and leaking seals.
- Layout: allow access for cleaning, maintenance and changeover, and keep product flow in one direction without backtracking.
- Safety: guarding and safety functions follow EN 415 for packaging-machine safety and your site lockout/tagout rules. Confirm interlocked guards and e-stop zones before commissioning.
Step 6 — Integration and controls
Agree how the machines talk: a simple line-stop signal, or a line controller and MES with recipe, traceability and OEE reporting. The controls scope should match the operators who will run it — a line that needs an engineer to change SKUs fails the first time the engineer is on holiday.
Step 7 — Acceptance before you pay the balance
Put the acceptance criteria in the purchase order: a witnessed trial on your product, a measured rate, a defined reject rate, and signed FAT and SAT protocols. See FAT and SAT for Packaging Machinery for the full protocol. If the line has multiple suppliers, one integrator must own the interfaces — the gap between two vendors’ machines is the gap that stops the line.
| Design stage | What to fix before the next stage |
|---|---|
| Product & format | Product behaviour, container, closure, secondary pack |
| Rate | Sustained good packs/min + 10–20% headroom |
| Sequence | Primary → secondary → end-of-line order |
| Balance | Bottleneck, buffers, inspection position |
| Utilities & safety | Air, power, water, layout, EN 415 guarding |
| Acceptance | FAT/SAT criteria written into the PO |
Frequently asked questions
Should I buy a complete line or integrate separate machines?
Buy a complete line when one supplier owns the whole scope and your formats are stable. Integrate separate best-of-breed machines when you need a specialist filler or sealer, and appoint one integrator to own every interface.
How much headroom should a line have?
Size for a sustained rate 10–20% above your committed output. More headroom than that usually means you bought speed you will never use; less means any stoppage eats into your order book.
Where should inspection sit on the line?
Downstream of the operation that creates the defect — after filling for fill errors, after sealing for seal defects — so rejects are caught before the pack reaches the case packer.
Source: Package testing — Wikipedia
"Package testing or packaging testing involves the measurement of a characteristic or property involved with packaging."
Related guides
- End-of-Line Machines: Top 10 Compared (2026) — Ten end-of-line machines compared across case packing, palletizing, sh…
- Case Packing vs Palletizing: Which to Automate First — case packing and palletizing are two different automation decisions — …
- Conventional vs Robotic Palletizing — conventional (layer) palletizers build a whole layer at once and win o…
- Shrink Wrapping vs Stretch Hooding — shrink wrapping and stretch hooding both stabilize a pallet load with …
- FAT and SAT for Packaging Machinery: Acceptance Testing Explained — FAT and SAT are the two acceptance gates that transfer risk from the s…
- Packaging Line OEE and Downtime Analysis: Measure the Losses That Matter — OEE turns a vague “the line is down too much” into three m…
- How a Case Packer Works — a case packer takes individual packs and builds them into a shipping c…
- How a Robotic Palletizer Works — a palletizer takes cases or packs and builds them into a stable pallet…
Last verified: October 20, 2026.