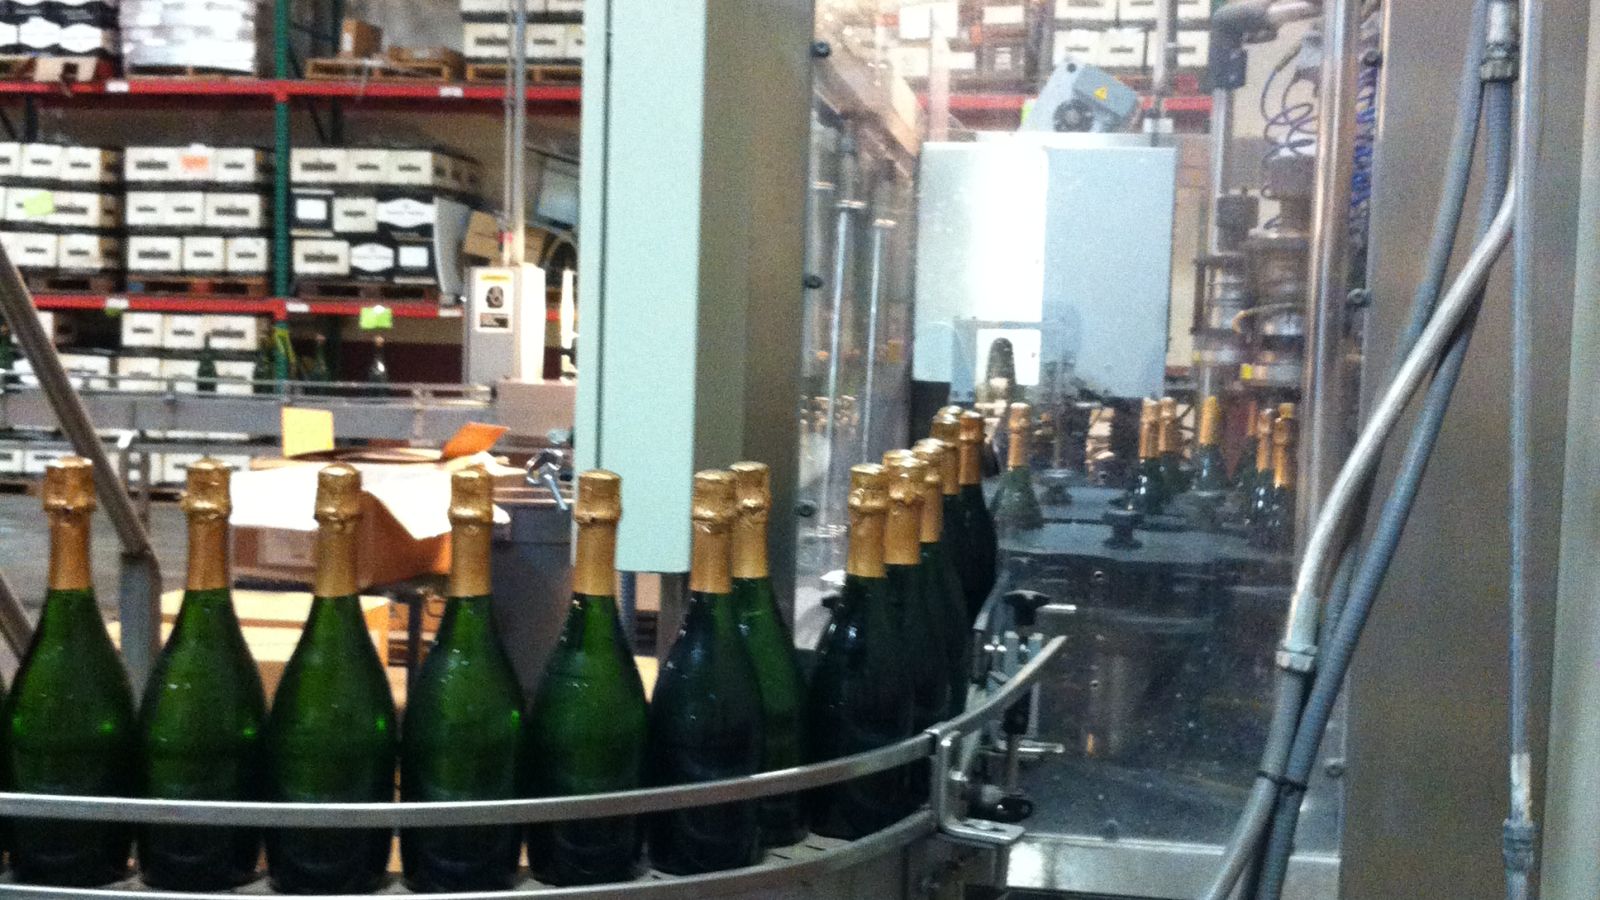
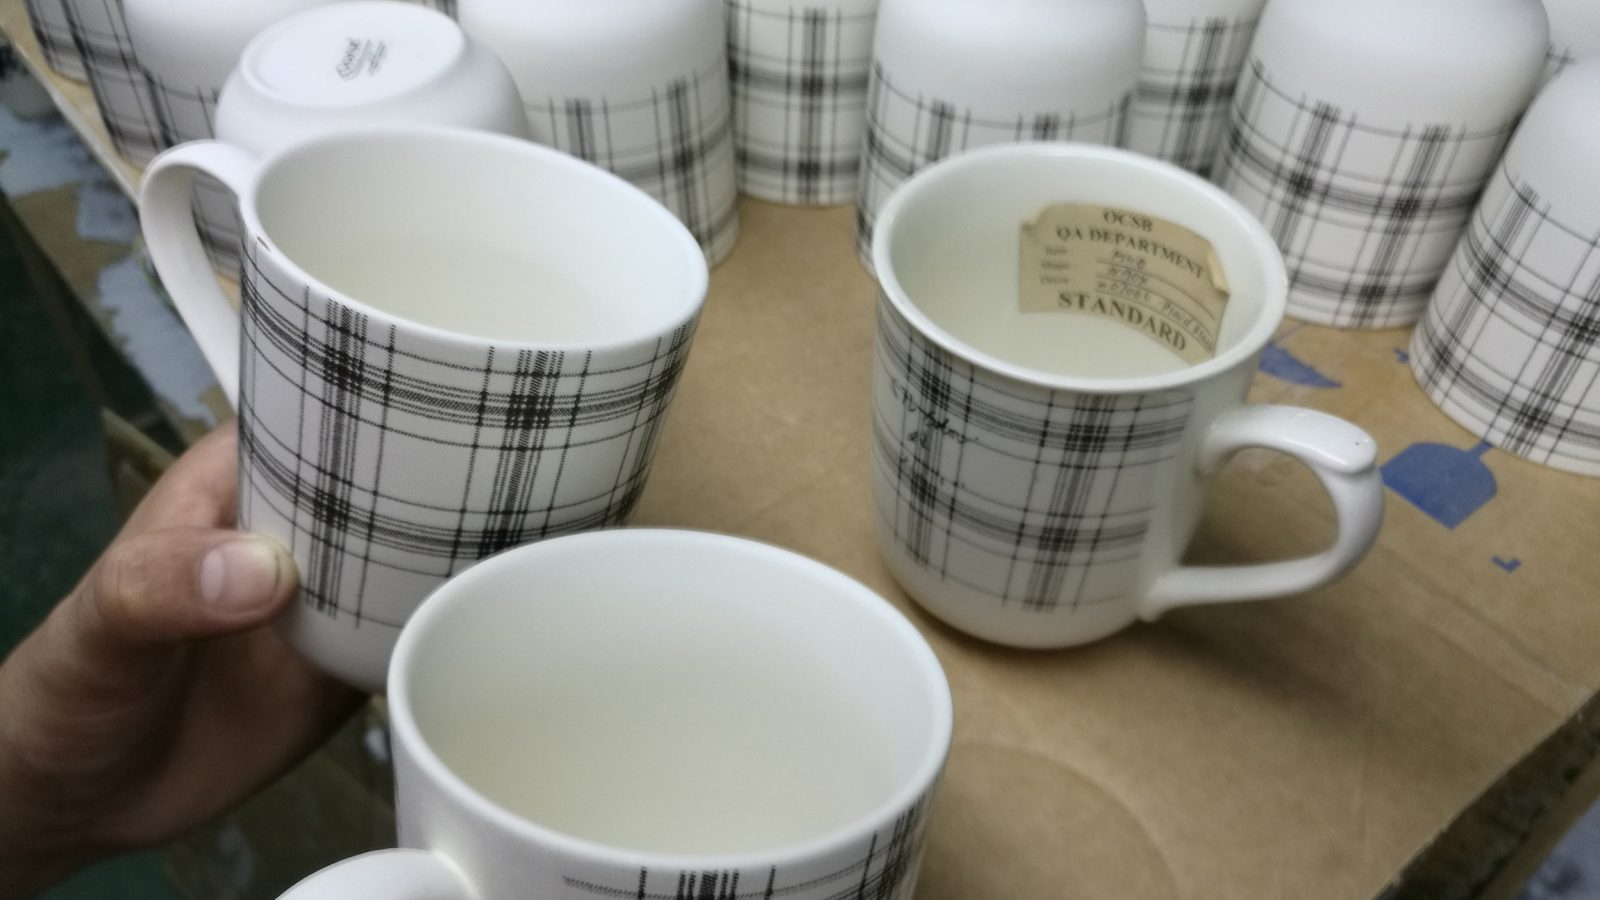
The core idea of this page: the factory acceptance test is the last moment when fixing a problem is cheap. Once the machine is crated, the cost of every defect multiplies — transport, rigging, lost production, a second visit. A FAT is not a demonstration; it is a structured test against criteria agreed in advance, witnessed by the buyer, with results written down.
What a FAT must cover
Mechanical build and materials
Frame, guards, contact parts and surface finish against the specification: stainless grade, weld finish, product-contact material certificates, and whether the machine is washdown-rated or dry-clean only. Photograph the nameplate and serial number.
Electrical and controls
Panel build against drawings, component brands as specified, sensor and safety-device list, PLC and HMI software version, recipe storage, and alarm list. Confirm the safety functions: interlocks, guard switches, emergency stop category and stop time where relevant.
Functional sequence
Run every motion in manual, then in automatic, then in the actual production sequence. Test the states that are easy to forget: empty-line start, starved infeed, blocked outfeed, power recovery, and a mid-cycle stop with product in the machine.
Performance against rated output
Run at rated speed for a sustained period with the buyer's own product and packaging material. Sustained means long enough to see thermal drift and to catch small stops — typically hours, not minutes. Record output, stops, rejects, and the reasons.
Watch for the pattern that a short demonstration always hides: the first thirty minutes run clean, then seal temperature drifts, film tension wanders or a sensor collects dust and the small stops begin. A one-hour test sees none of it. Attach the stop log to the report, with each stop classified, so the buyer can judge whether the line meets rate in steady state or only in its first hour.
Pack quality
Measure what the product requires: fill weight and giveaway, seal strength and appearance, leak rate, label position, code legibility, case pattern. Agree the sampling plan and the acceptance limits before the test, not after seeing the results.
Documentation and spares
Drawings, manuals, spare-parts list, recommended spares, calibration certificates, material certificates and the CE or equivalent declaration. A machine that passes the test but arrives without documentation fails the project.
How to write acceptance criteria that hold up
Criteria must be numeric, measurable on the day, and traceable to the purchase specification. "Seals must be strong" is not a criterion; "seal strength not below the agreed value on the agreed sample size, measured by the agreed method" is. Every criterion needs a method, a sample size and a pass limit. Where the buyer and supplier disagree on method, settle it at contract stage, because arguing about method during the FAT is how tests get waived.
The punch list and the retest
Every deviation found during the test goes onto a punch list with three fields: what is wrong, who fixes it, and when it will be retested. Separate cosmetic items from functional ones, because mixing them lets a missing safety interlock wait behind a paint touch-up. Agree the retest scope in writing on the day — a full rerun, or a targeted test of the affected function with a witness.
A punch list that closes verbally is the single most reliable predictor of a painful site acceptance test. If the supplier cannot give a date, the machine should not ship.
Who attends and for how long
At minimum: the buyer's project engineer, the future operator or maintenance lead, and quality. Budget enough days to run the full sequence twice — once to find the problems, once to prove the fixes. A one-day FAT on a multi-format line is a demonstration, not a test.
FAT versus SAT
The FAT happens at the supplier's works on their utilities and often their material; the site acceptance test happens after installation on the buyer's utilities and product. Passing the FAT does not guarantee the SAT, because utilities, ambient conditions, product variability and line integration only appear on site. Plan both, with separate criteria.
What a skipped or hollow FAT costs
The economics are simple. A defect found at the supplier's works costs a few hours of engineering time. The same defect found on site costs transport, rigging, a technician visit, lost production during the fix and a second acceptance test — and it lands during the ramp-up window when the plant is least able to absorb delay. The FAT is the cheapest test the project will ever run.
Failure modes that hollow out a FAT
Testing at reduced speed, testing with material the buyer will never use, testing only the easiest format, and accepting verbal fixes with no retest. Another common one: the buyer sends nobody with authority to sign, so the test ends with "looks fine" and the punch list never closes.
Verification checklist
Before signing: every criterion has a recorded measured value; the machine configuration matches the drawings and the agreed option list; every safety device has been function-tested and the test recorded; the punch list is written with owners and dates; rejected packs are retained and counted; the sustained run duration and stop log are attached; documentation is complete; and the retest scope is agreed for every open item.
Source: Acceptance testing — Wikipedia
"In engineering and its various subdisciplines, acceptance testing is a test conducted to determine if the requirements of a specification or contract are met."
Frequently asked questions
Who pays for the FAT?
The buyer normally bears travel and their own staff time; the supplier bears running the machine, material and retests. Agree this in the contract, because retest costs are where disputes start.
Can a FAT be waived?
Only with a written risk acceptance. Waiving removes the cheapest opportunity to find defects and usually moves the cost to the SAT, where schedule pressure is higher.
How long should the sustained run be?
Long enough to reach thermal stability and to expose small stops — commonly four to eight hours per format, longer for high-speed lines.
Related reading: FAT and SAT guide, site acceptance test, line design and integration, and the end-of-line packaging category.
Related guides
- End-of-Line Machines: Top 10 Compared (2026) — Ten end-of-line machines compared across case packing, palletizing, sh…
- Case Packing vs Palletizing: Which to Automate First — case packing and palletizing are two different automation decisions — …
- Conventional vs Robotic Palletizing — conventional (layer) palletizers build a whole layer at once and win o…
- Shrink Wrapping vs Stretch Hooding — shrink wrapping and stretch hooding both stabilize a pallet load with …
- Packaging Line Design and Integration Guide: Plan a Line That Runs — a packaging line is designed from the product out, not from the machin…
- FAT and SAT for Packaging Machinery: Acceptance Testing Explained — FAT and SAT are the two acceptance gates that transfer risk from the s…
- Packaging Line OEE and Downtime Analysis: Measure the Losses That Matter — OEE turns a vague “the line is down too much” into three m…
- How a Case Packer Works — a case packer takes individual packs and builds them into a shipping c…